Short answer: metal disappears continuously in a working shop — into sprues and buttons, bench filings, polishing dust, floor sweeps, aprons, rags and sink traps — and it is recovered later through refining. What almost nobody can tell you is how much is lost at each stage, because no one publishes that. What is published is what each type of scrap yields when you send it in, and that is enough to build a measurement habit of your own.
The goal of this piece is to replace a number you have heard with a number you can prove.
The table that doesn't exist
If you have ever gone looking for "casting loses X percent, filing Y percent, polishing Z percent," you will not find it. We checked Ganoksin, Stuller's Bench Jeweler library, Rio Grande, MJSA and the Santa Fe Symposium archives. A stage-by-stage loss percentage breakdown is not published in the English-language trade literature.
That is worth stating plainly because the absence gets filled with folklore. Shops run on numbers someone was told years ago, and those numbers quietly set costing allowances and scrap expectations for a decade.
Two things circulate that look like the missing table but are not.
The first is the Indian wastage percentage — figures like 3 to 7 percent for 22k, 6 to 12 percent for 18k, quoted in ranges by design complexity. These are a retail pricing convention levied on the customer, not a measurement of unrecovered metal in a workshop. They are not comparable to a Western manufacturer's loss rate and should not be used as one.
The second is a single anecdote from a refining equipment vendor describing an unnamed company whose polishing room alone was responsible for a 3 percent annual loss, reduced by 80 percent after upgrading suction and retraining staff. It is vendor marketing with no methodology and no named company. It is interesting as a shape — polishing is a big contributor, extraction and training help — but it is not a benchmark.
What is published: yields by scrap type
Here the sourcing is solid, and it is genuinely useful. Stuller publishes approximate gold recovery yields by material:
| Material | Approximate yield |
|---|---|
| Clean filings | ~40% fine gold by weight |
| Dirty bench sweeps | ~5% to 20% fine gold by weight |
| Buffing dust | ~2% fine gold by weight |
| Floor sweeps, including vacuum bags | ~1% by weight |
Ganoksin's figures for polishing sweeps sit alongside these: 14k manufactured polishing sweeps can yield as much as 4 percent. For platinum polishing sweeps the assayed content ranges from around 0.5 percent up to roughly 8 percent, with the low end caused by mixing gold dust with platinum dust in the same refining lot — a costly, avoidable mistake.
Read that table as a hierarchy of care. Clean filings are worth twenty times what an equivalent weight of buffing dust is worth, and forty times what floor sweeps are. Everything you do to keep filings clean and separate from everything else is high-return work; everything that lets filings end up in the general sweep destroys most of their value.
The sink trap, with an actual number
The most quotable measured datapoint in the published literature is small and specific. Stuller reports that after nearly six weeks of using a drain sweeper, 0.082 ounces of gold were recovered.
They priced it at $77.67 at a gold price of $947.25, which dates that figure to roughly 2009. Ignore the dollar amount and keep the ounces: 0.082 troy ounces in six weeks, from one shop's sink. Multiply 0.082 by today's spot and by roughly eight and a half to annualise, and you have a straightforward answer to whether a drain trap pays for itself.
Where the rest of it goes
Refiners will take far more than most benches send them. Garfield's published list of acceptable sweeps material is instructive because of how mundane most of it is: grindings, shavings, cuttings, sandpaper, polishing wheels, emery sticks, flex shaft bits, dust masks, broken saw blades, sludge from ultrasonic cleaners, carpet and flooring, vacuum bags, collection bags from dust and fume collectors, paper towels, brushes, rags and gold-filled jewelry. Elemetal categorises low-grade as bench sweeps, floor sweeps, grindings, filings, polishings, filters and sink collections.
Two things follow. First, most shops are throwing away several of those categories. Second, when it comes time to ship, weight matters — because refining charges on sweeps are calculated against the incoming weight of the material. Ganoksin's practical tip is to pull steel out with a magnet before shipping, reducing the weight of the lot and lowering the refining cost. Free money, five minutes.
On grading, Arthur Anton Skuratowicz's summary is that companies which refine sweeps pay higher for clean sweeps than dirty sweeps. And the realistic framing from the same article, which is worth keeping in view before anyone buys a $4,000 extraction system: "you will never be able to capture and refine every single speck of metal that enters your shop."
Casting: reuse before you lose
Not all metal that leaves a job is lost. Ganoksin's guidance on casting reuse is that many gold manufacturers can go as many as 1 to 15 casting lots by refreshing before starting with completely new casting grain, with 50 to 75 percent new gold alloy required to maintain purity and karatage. Platinum is far more forgiving: reuse and addition of new alloy can be done 40 to 50 times without problems before scrapping material for refining.
Investment is the other casting-side recovery. A 1987 Santa Fe Symposium paper by Dave Schneller on recovering precious metals from used casting investment found that most of the gold is contained in about 5 percent of the investment, in the largest mesh sizes. The same paper warns that assays of investment are unreliable due to the nugget effect from large metallic particles, and that the recovery figures reported should be regarded as preliminary. Treat investment recovery as worth screening for, not as a precise science.
Measuring your own rate
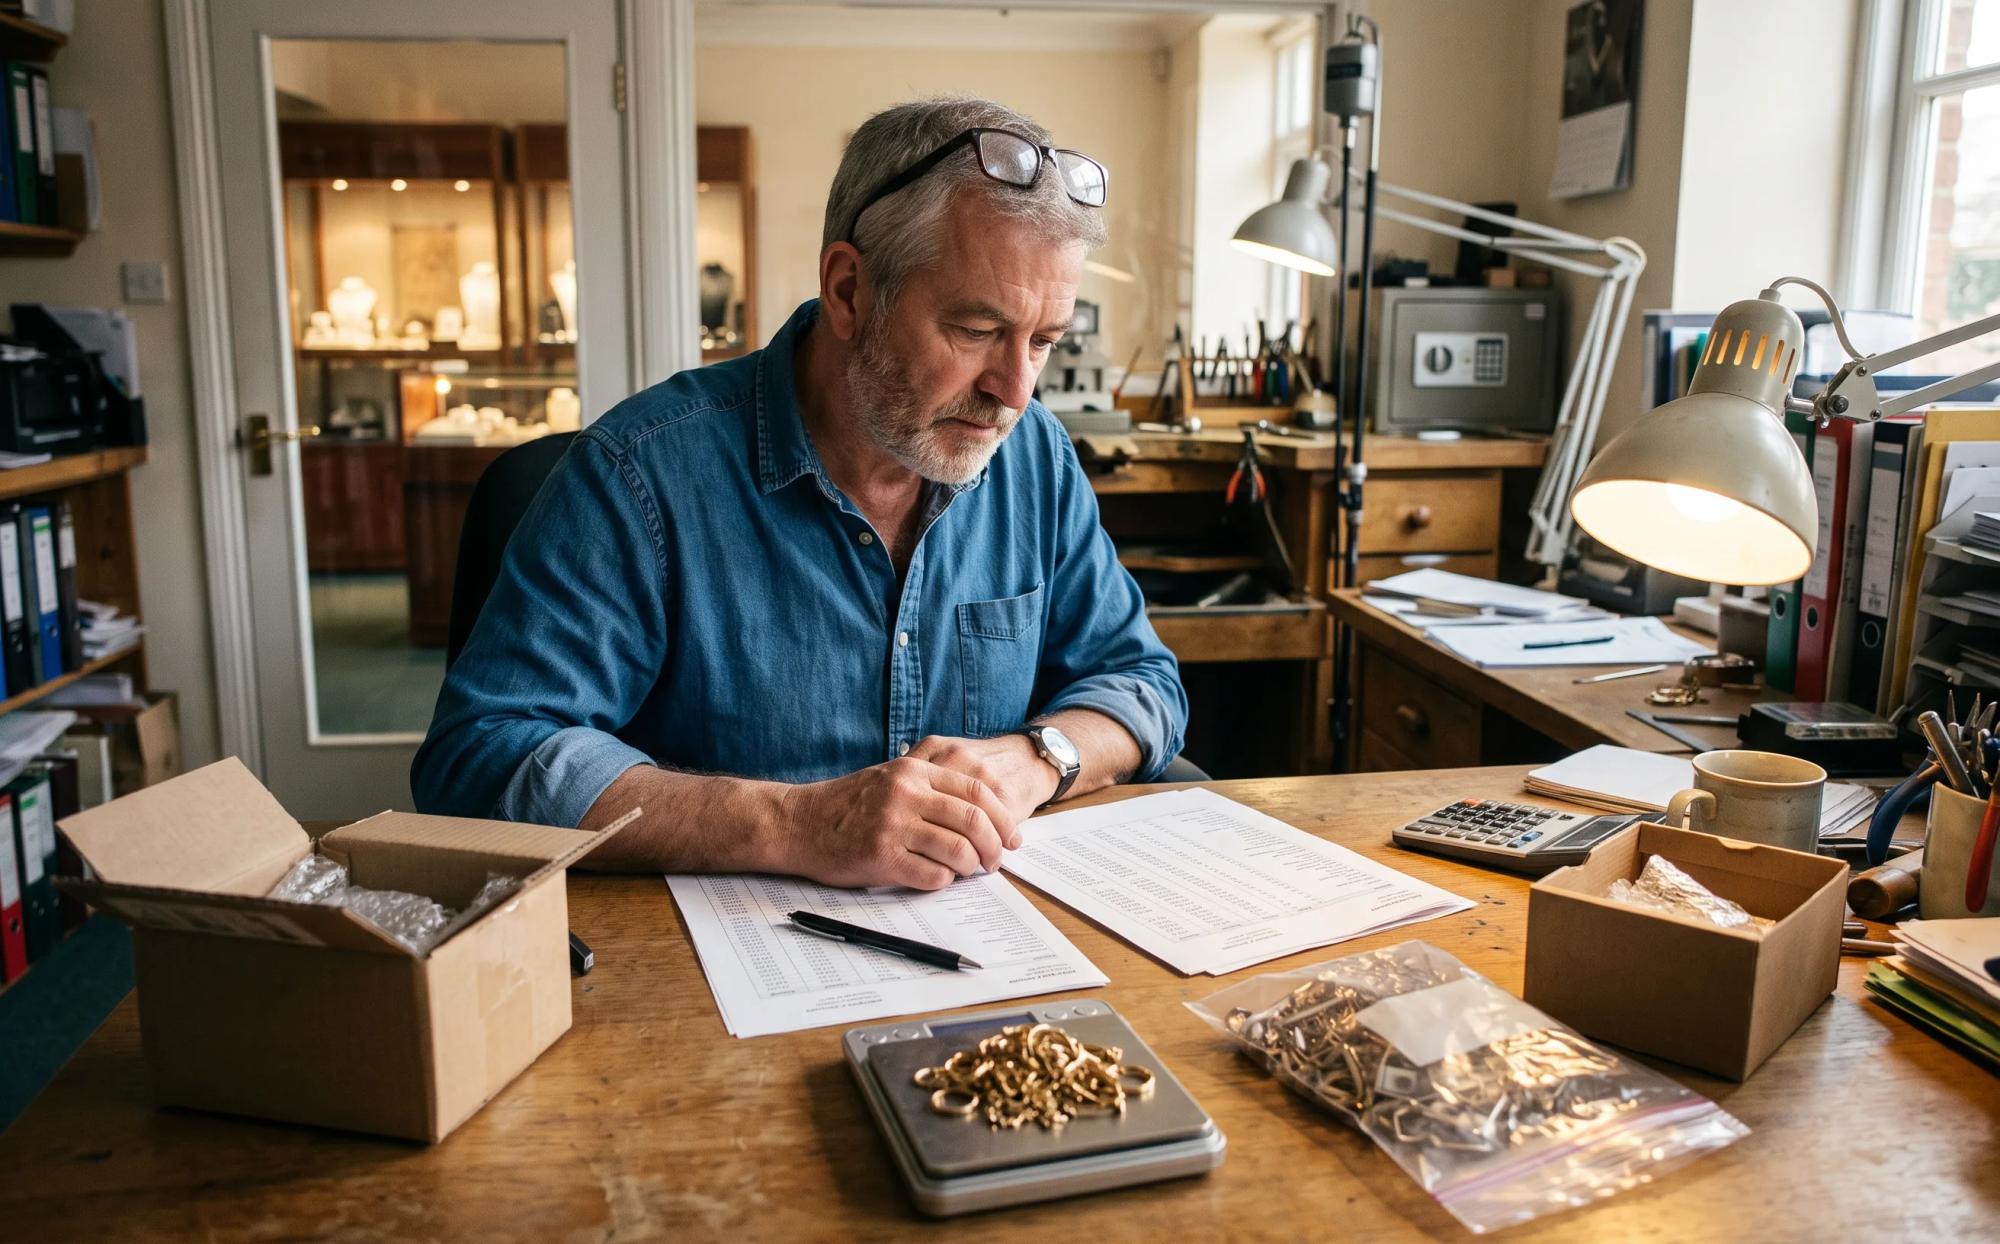
Since the industry figure does not exist, build yours. It takes three weights per job and a habit.
Weigh metal issued. Grain, sprue, or stock, recorded against the job before work starts.
Weigh the finished piece. After final finishing, before it leaves.
Weigh recoverable scrap returned to the job. Sprues, buttons and clean filings that are identifiably from that job.
Loss is issued minus finished minus recovered. One job tells you nothing. Thirty jobs of similar type tell you a rate, and that rate is specific to your alloys, your casters, your polishers and your extraction — which makes it worth more than any published figure could be.
The rate then does real work. It gives you a defensible allowance to build into job costing rather than a guess. It gives you a baseline against which a sudden change means something — a new polisher, a worn extraction filter, or metal walking out of the door. And it gives you a number to put against the cost of better collection, so the extraction argument becomes arithmetic rather than instinct.
A note on that last point: no published trade source specifies a casting-loss allowance to add into a job cost. Ganoksin's own costing articles charge metal at actual weight, at keystone of cost at that day's price, without a stated loss uplift. So if you want an allowance in your costing, you have to measure it.
Where Jewelia fits
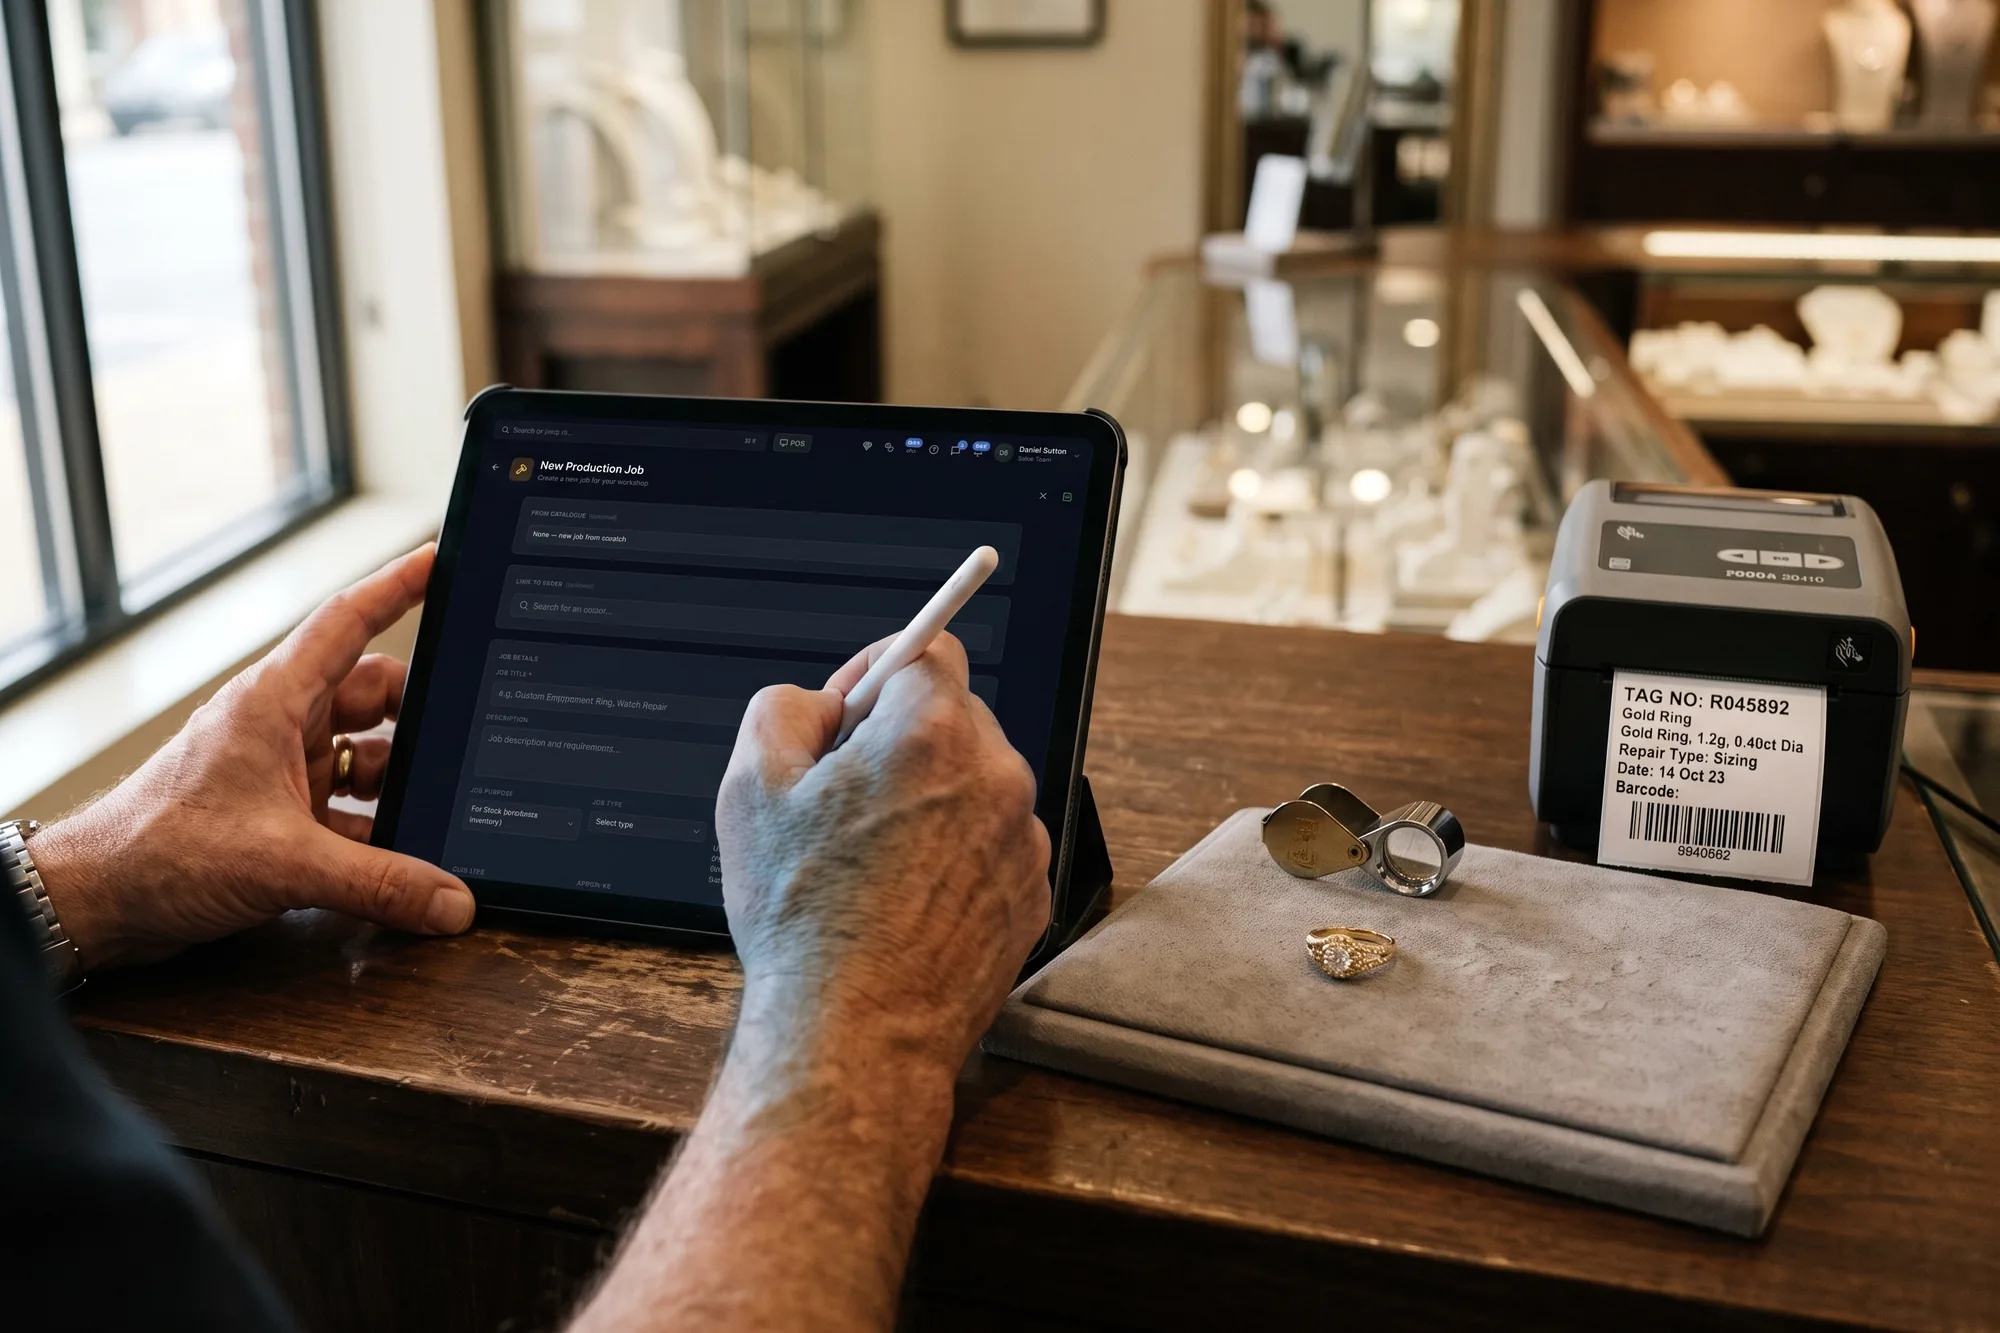
Measuring loss per job only works if the weights land somewhere they can be compared. Production & Repairs records materials against the job as the work happens, with configurable stages and forms completed at each one, so issued weight, finished weight and returned scrap are fields on the record rather than notes on a bag. Metal, karat, weight and fineness live on items in inventory, so materials are drawn against real specifications rather than estimated.
Once the data is there, analytics makes it a rate: loss by job type, by stage and by person, across enough jobs to mean something. That is the point at which a shop stops arguing about whether polishing is costing them and starts knowing. Inventory also reports a replacement valuation at today's metal spot prices alongside cost, which is the other half of understanding what the metal in your building is worth right now.
Bottom line
There is no published per-stage metal loss table, so stop looking for one. There are published yields: clean filings around 40 percent, dirty bench sweeps 5 to 20, buffing dust about 2, floor sweeps about 1 — which tells you that keeping filings clean and separate is the highest-value habit in the shop. Magnet the steel out before you ship. Trap the sink. Reuse casting metal within sensible limits. And weigh issued, finished and returned against every job until you have a loss rate that is actually yours.
Frequently asked questions
- How much metal is typically lost in jewelry manufacturing?
- There is no published per-stage loss table for casting, filing, polishing and setting — we looked at Ganoksin, Stuller's Bench Jeweler library, Rio Grande, MJSA and the Santa Fe Symposium and found none. What is published is the inverse: recovery yields by scrap type. Anyone quoting you a confident industry loss percentage per stage is quoting something they cannot source.
- What are bench filings and sweeps actually worth?
- Stuller publishes approximate gold recovery yields: clean filings around 40 percent fine gold by weight, dirty bench sweeps roughly 5 to 20 percent, buffing dust around 2 percent, and floor sweeps including vacuum bags around 1 percent. Ganoksin reports 14k manufactured polishing sweeps yielding as much as 4 percent.
- Is it worth putting a trap on the sink?
- Stuller reports a measured result: after nearly six weeks of using a drain sweeper, 0.082 ounces of gold were recovered. That was worth about $78 at the gold price of the day, which dates the figure — recompute 0.082 ounces at today's spot to see what six weeks is worth in your shop.
- Can I recover metal from used casting investment?
- Some. A Santa Fe Symposium paper on recovering precious metals from used casting investment found that most of the gold is contained in about 5 percent of the investment, in the largest mesh sizes. The same paper warns that assays of investment are unreliable because of the nugget effect from large metallic particles.
- How do I work out my own metal loss rate?
- Weigh metal issued to a job, weigh the finished piece, weigh recoverable scrap returned, and record all three against the job. Loss is what is left. Do that consistently across enough jobs and you have a rate specific to your shop, your alloys and your processes — which is worth far more than a borrowed industry number.
- Is Indian 'wastage percentage' the same as metal loss?
- No, and conflating the two is a common error. Wastage charge in the Indian retail trade is a pricing convention levied on the customer, typically quoted in ranges by karat. It is not a measured record of unrecovered metal in a workshop and is not comparable to a Western manufacturer's actual loss rate.
Stop reading, start clicking.
Open a live Jewelia company with real inventory, memo, jobs and reports already in it. One work email, no card, no sales call, nothing to install.